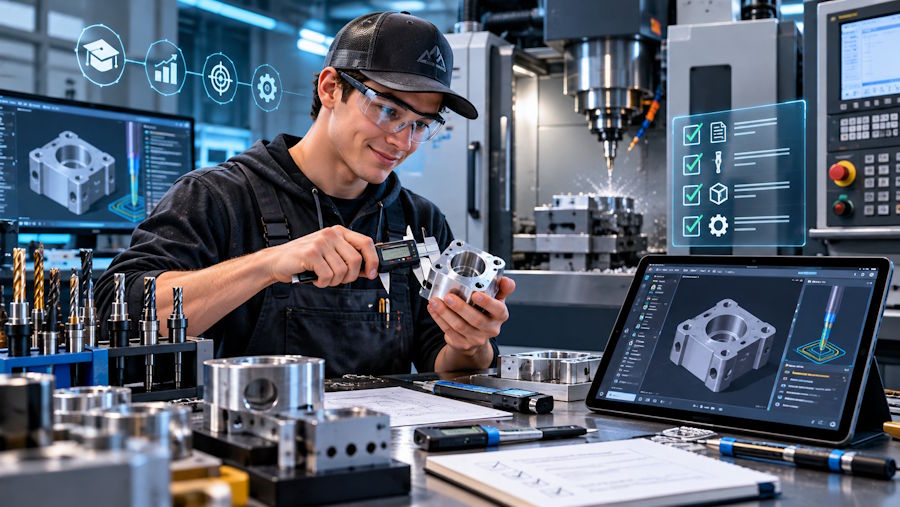
Walking into a machine shop for the first time can feel overwhelming. Between the machines, cutting tools, measuring instruments, and unfamiliar terminology, there is plenty to learn before you finish your first part. Building confidence starts with understanding a few essential tools and developing a dependable routine for using them.
For beginners working with round stock, lathe tools provide a practical introduction to machining fundamentals. Turning a diameter, facing an end, and creating a simple shoulder teach you how tool position and cutting conditions affect the finished workpiece. Each operation also creates an opportunity to connect the drawing to something you can measure.
Inspection equipment helps complete that learning process. Checking heights and hole sizes gives you useful feedback about your setup and machining decisions. Instead of judging a part only by its appearance, you can verify whether its features meet the drawing. That combination of careful cutting and consistent inspection helps new machinists develop confidence grounded in results.
Get Comfortable With Basic Lathe Tooling
A lathe rotates the workpiece while a cutting tool removes material. Although that basic principle is straightforward, different operations require different tool shapes and approaches. Before selecting a tool, review the drawing and identify the outside diameters, faces, shoulders, grooves, and holes the part requires.
Start with a manageable project. A simple stepped shaft or spacer can introduce facing, outside turning, and dimensional checks without adding complicated geometry. Choose a project that matches your machine, available tooling, and level of instruction. Fewer features make it easier to understand why a cut behaves the way it does.
Facing is often an early operation because it creates an end surface that can serve as a reference for later work. Outside turning reduces the workpiece diameter, while shoulder machining creates transitions between different diameters. Learning the purpose of each operation helps you organize the job into a logical sequence.
Tool selection should account for the workpiece material and the specific cut. Insert geometry, cutting-edge strength, and recommended cutting conditions all influence performance. A tool suited to finishing an accessible outside diameter may not be appropriate for a groove or an internal feature. Check the manufacturer's application guidance before assuming tools are interchangeable.
Proper positioning matters just as much as selection. Set the cutting edge at the appropriate center height and confirm the holder's orientation and clearance. Incorrect positioning can affect cutting behavior and the resulting surface. Follow the machine and tooling instructions, and have an experienced machinist review unfamiliar setups before cutting.
Rigidity is another foundation of dependable lathe work. Keep tool overhang as short as practical and use suitable workholding for the stock. Long or slender workpieces may require additional support, depending on the operation. Check that the setup can resist cutting forces without allowing the material or tool to shift.
Before starting the spindle, verify clamping, clearances, and the machine's operating limits. Remove the chuck key if your machine uses one, secure loose clothing and hair, and follow shop rules for eye protection. Never reach toward rotating stock or attempt to measure a moving workpiece. Stop the machine before inspecting or making adjustments.
As you begin cutting, pay attention to changes in sound, chip formation, and surface appearance while staying behind the machine's guarding. Unusual vibration or a sudden change in finish deserves investigation. Stop safely and check the setup instead of trying to compensate immediately with random speed or feed changes.
Keep a short record of the material, tool, cutting conditions, and measured results. Notes help you identify which adjustments improved the outcome. They also give you a useful starting point when a similar job comes along. Confidence grows faster when you can connect a successful result to a process you understand.
Bring Height and Hole Checks Into Your Routine
Inspection becomes more useful when it is part of the machining plan. Before making a part, identify the dimensions that control fit, alignment, or assembly. Decide when to inspect those features and which instruments are appropriate. This preparation helps you catch problems before later operations make them harder to correct.
For measurements referenced from a suitable flat surface, a height gauge can help check accessible feature heights. Used with a clean surface plate and the correct setup, it provides a consistent reference for inspection. Its usefulness depends on how the part is supported and whether the measurement matches the drawing's requirements.
Start by cleaning the surface plate, the part's supporting face, and the instrument's contact surfaces. Chips, dirt, and raised burrs can prevent the workpiece from sitting properly. Even a careful reading becomes unreliable when the reference surface underneath the part is wrong.
Check the instrument's zero or reference setting according to its instructions. Position the workpiece securely and bring the contact point to the feature using controlled, consistent technique. Avoid forcing the contact against the surface. Excessive pressure or unstable support can affect the reading and make repeated measurements disagree.
Remember that a measured height is only meaningful relative to its reference. A drawing may specify a dimension from a particular datum surface, so placing the part on a different face can answer the wrong question. Understanding that relationship helps beginners move beyond collecting numbers toward checking the features that matter.
Hole inspection requires similar care. A hole may need to provide clearance for a fastener, locate another component, or support a later operation. Those functions influence the acceptable size range and inspection method. Review the specified limits before deciding whether a hole is acceptable.
Near the end of your inspection routine, pin gauges can help assess accessible hole sizes through controlled fit checks. Select suitable gauge sizes based on the drawing and your inspection procedure. Gauge tolerance, condition, and the required acceptance criteria matter, particularly when checking close limits.
Clean the hole and gauge, remove interfering burrs appropriately, and never force a pin into place. A fit check does not establish every aspect of hole quality; location, straightness, and other geometric requirements may need separate inspection.
Building shop confidence comes from repeating sound habits. Learn a few basic lathe operations, establish reliable references, and check dimensions with suitable instruments. Record what worked and investigate inconsistent results. With each project, that routine helps you make better decisions and approach unfamiliar work with a stronger practical foundation.